Technology
The whole platform,
engineered in-house.
One printer, one slicer, one mix, all designed and built by the same team in Sydney.
One platform
Four parts, one platform.
Owning every layer of the stack is what lets us print real, occupied buildings, not prototypes, and shape concrete in ways conventional formwork cannot.
The printer
OPUS 4
Our own large format gantry printer.
Explore →The software
Contour Cloud
Control, slicing, quoting and live monitoring.
Explore →The material
ContourCrete
Our Australian made, eco-friendly print mix.
Explore →On-site systems
Batching & mixing
TITAN, MAI Multimix 3D and the bulk silo.
Explore →The second platform
Thermoplastic
Large-format pellet printing, in development.
Explore →Two materials
Concrete and thermoplastic.
The printer
OPUS 4
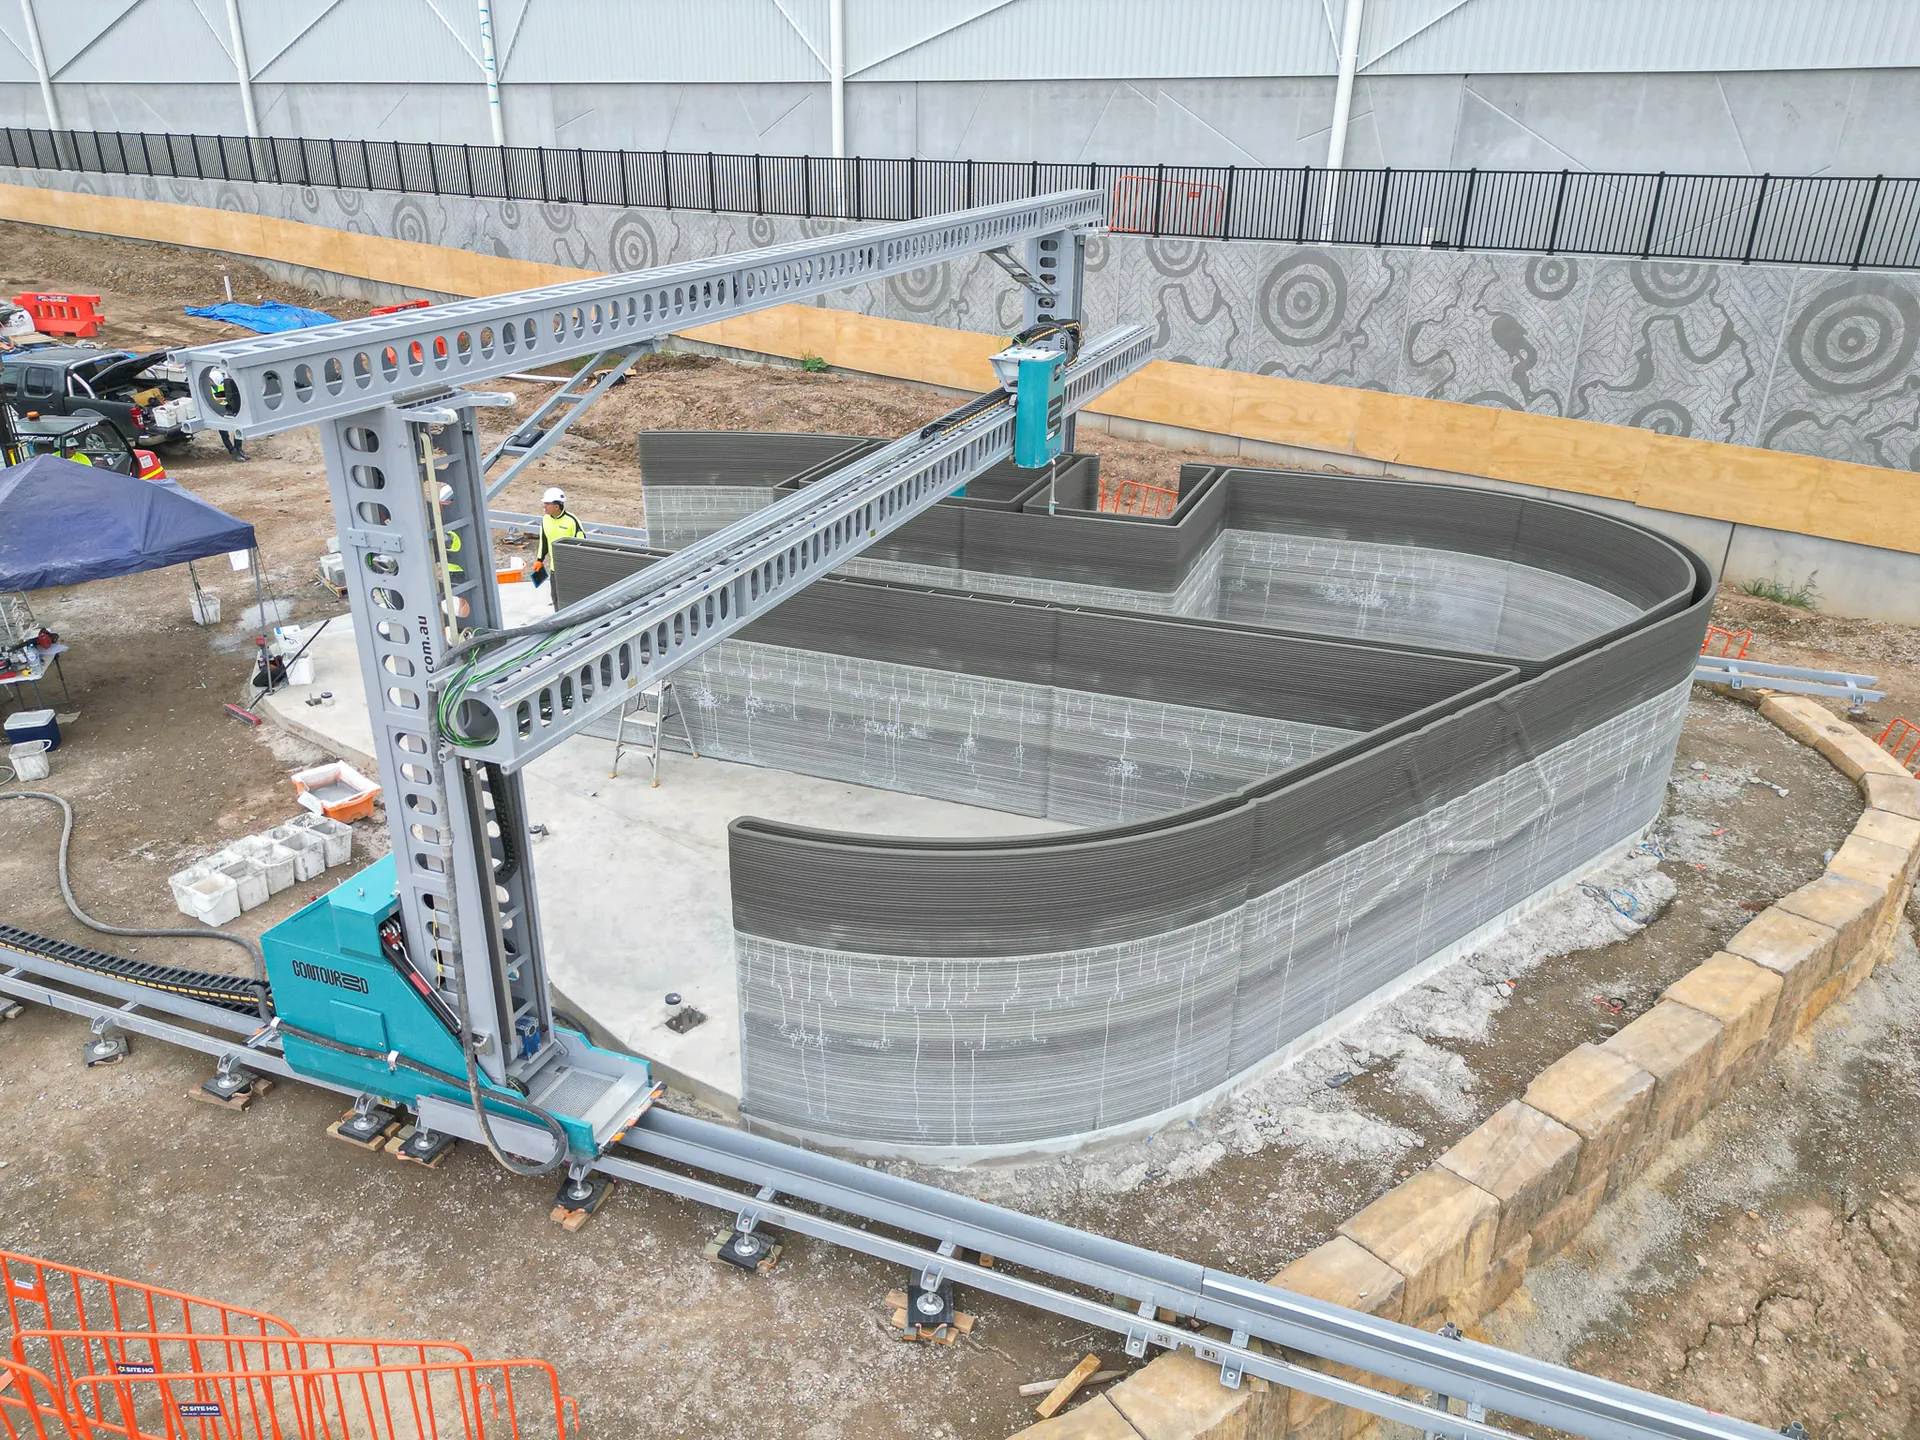
Our own large format gantry printer, engineered and built in-house.
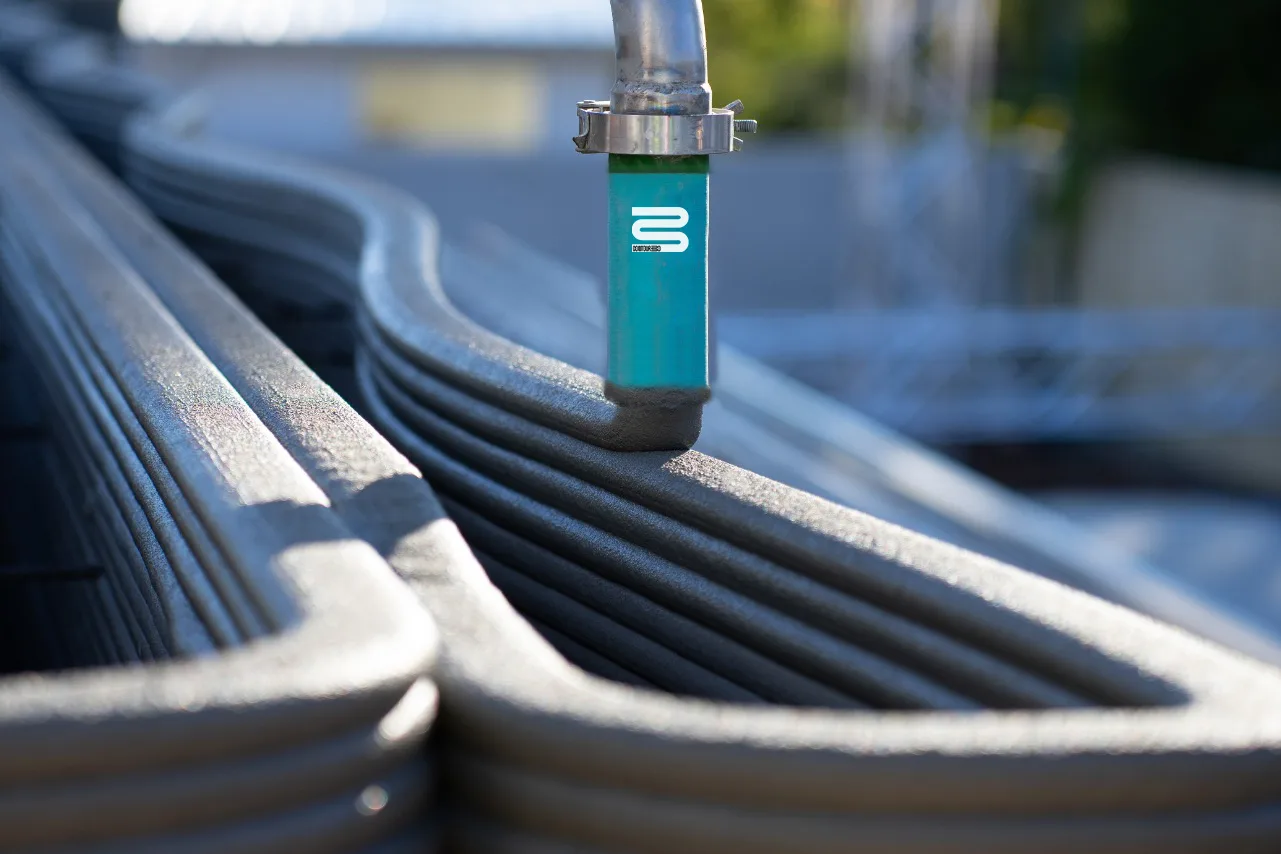
It lays ContourCrete bead by bead to form curved, structural walls on
site or in the factory, and it is the machine behind our printed
projects.
For fine detail work we run an ABB IRB 6640 robotic arm alongside it.
- Print method
- Large-format gantry, bead by bead
- Control system
- Contour Cloud
- Material
- ContourCrete
- Deployment
- On site or in the factory
The software
Contour Cloud.
Our own web-based platform connects the printer, the batching plant and
the control systems.
One secure login ties the whole job together: design, quoting, live
monitoring and support, connected over Starlink or 5G.
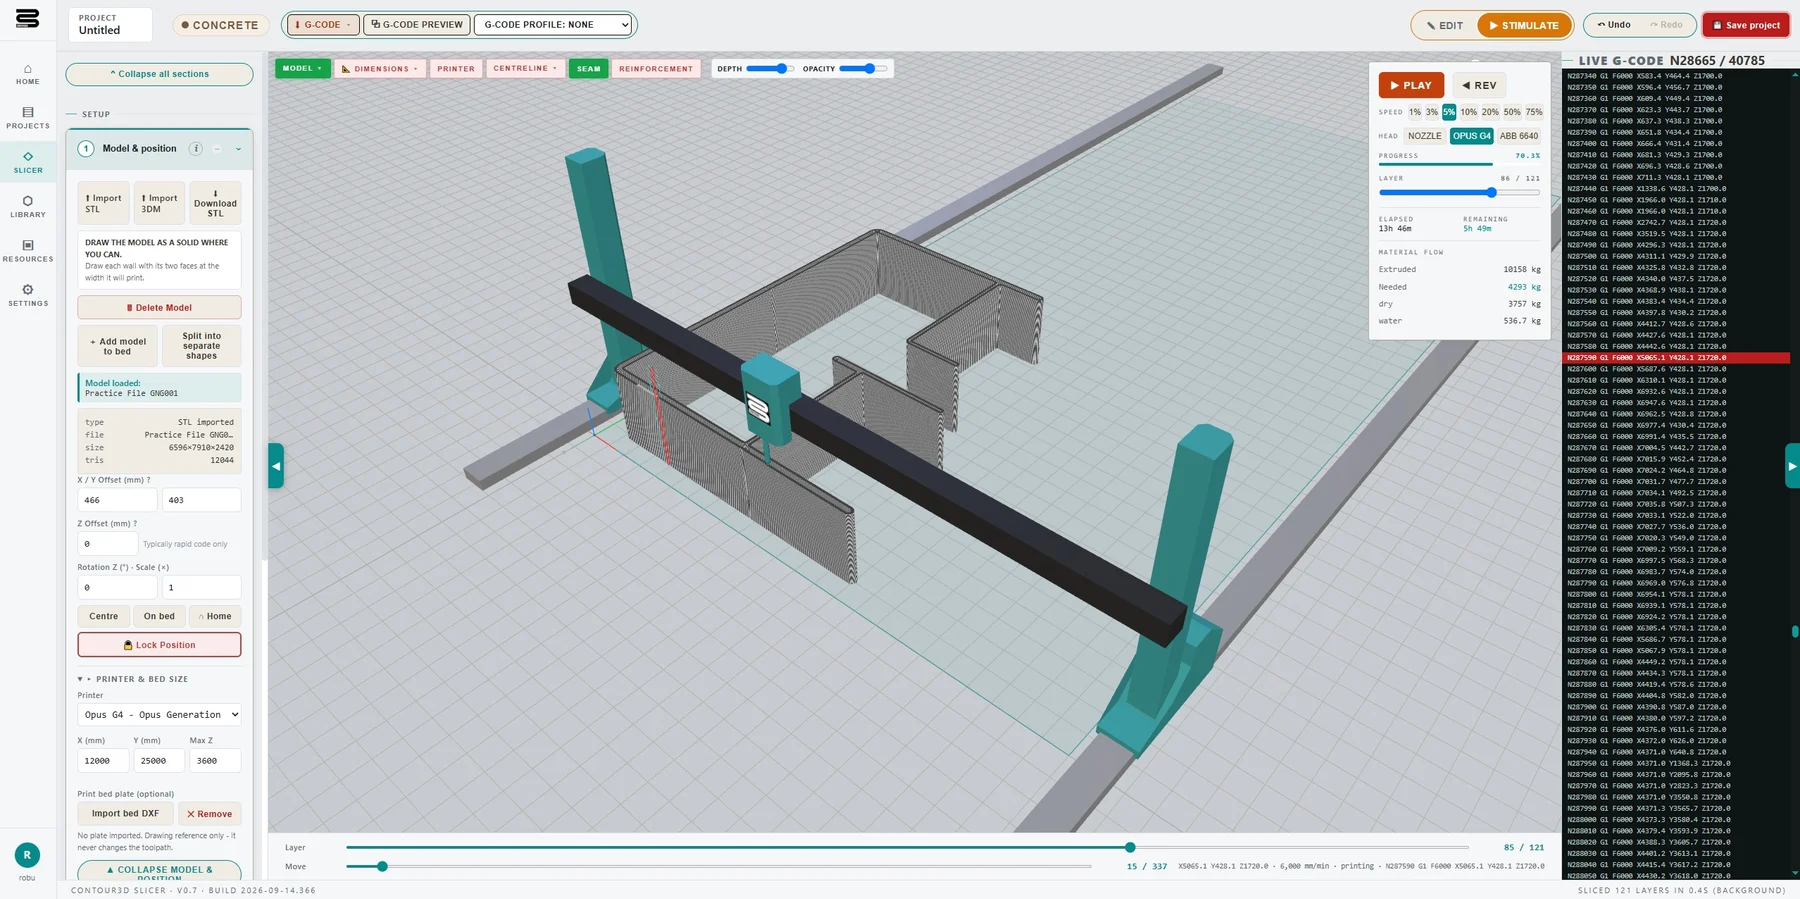
SliceMeUp
The slicer · by Contour3D
Slicing built for concrete rather than plastic.
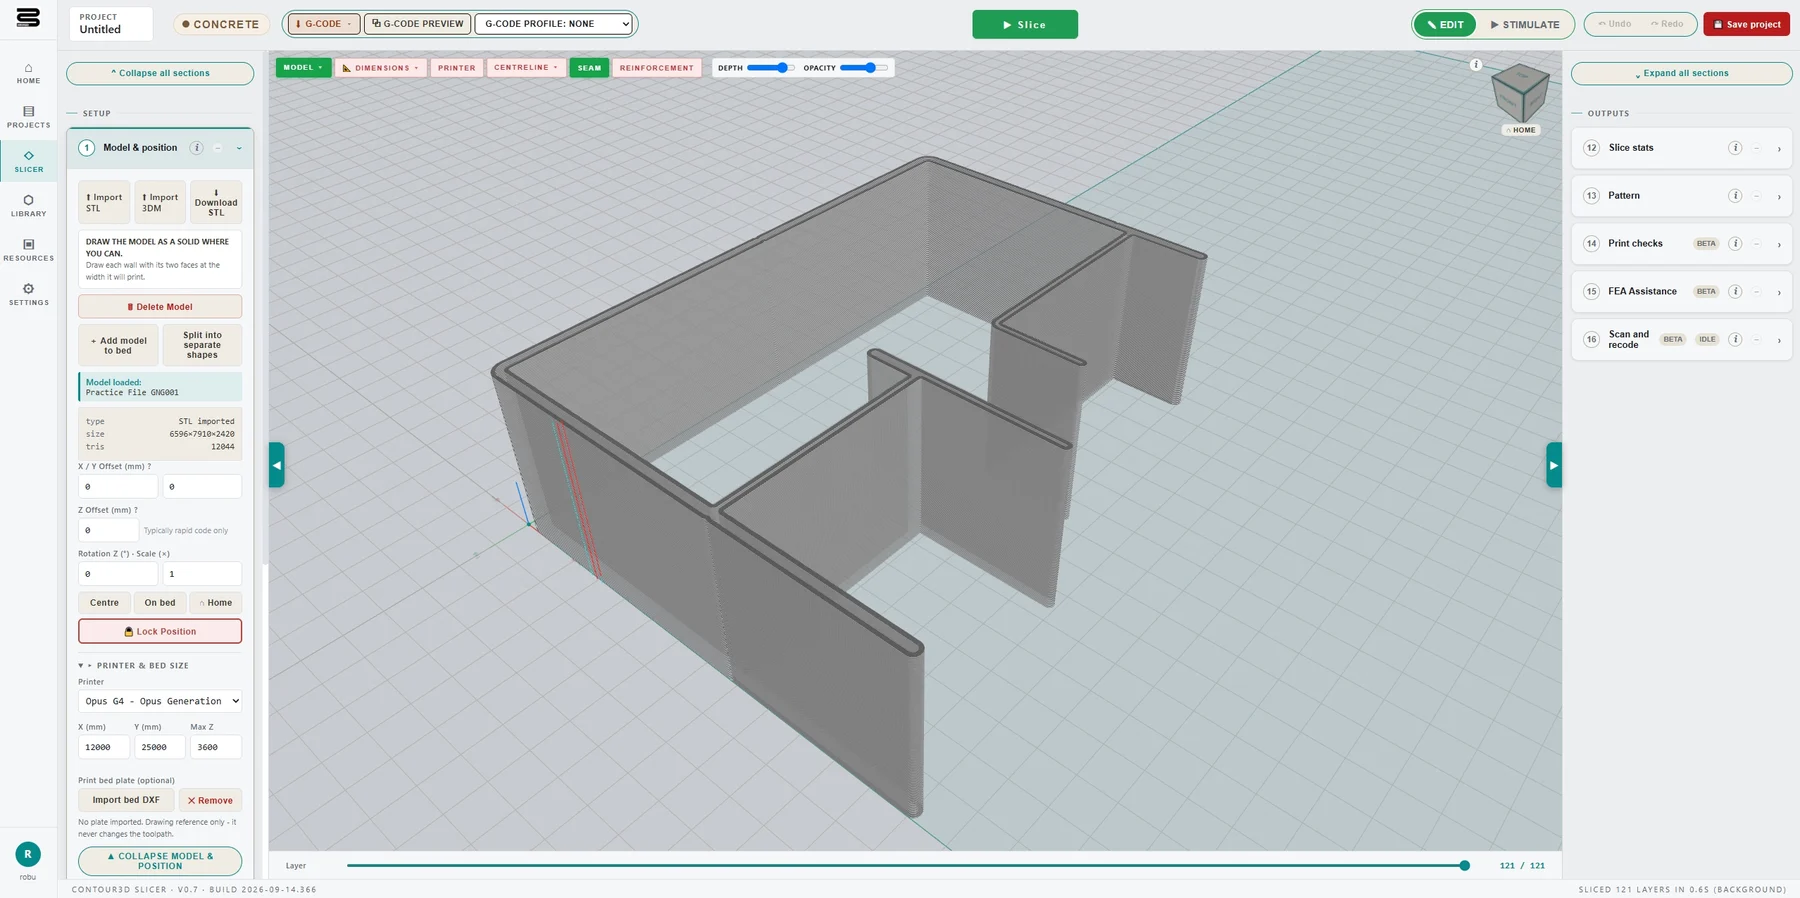
Slice Me Up turns a 3D model into a print-ready toolpath, checks it
will actually print, and optimises every layer before the machine
starts.
PriceMeUp
Instant quoting
Price a printed job in minutes. It reads the model to estimate print time, material volume, reinforcement and cost, so customers get a fast, consistent quote instead of waiting days.
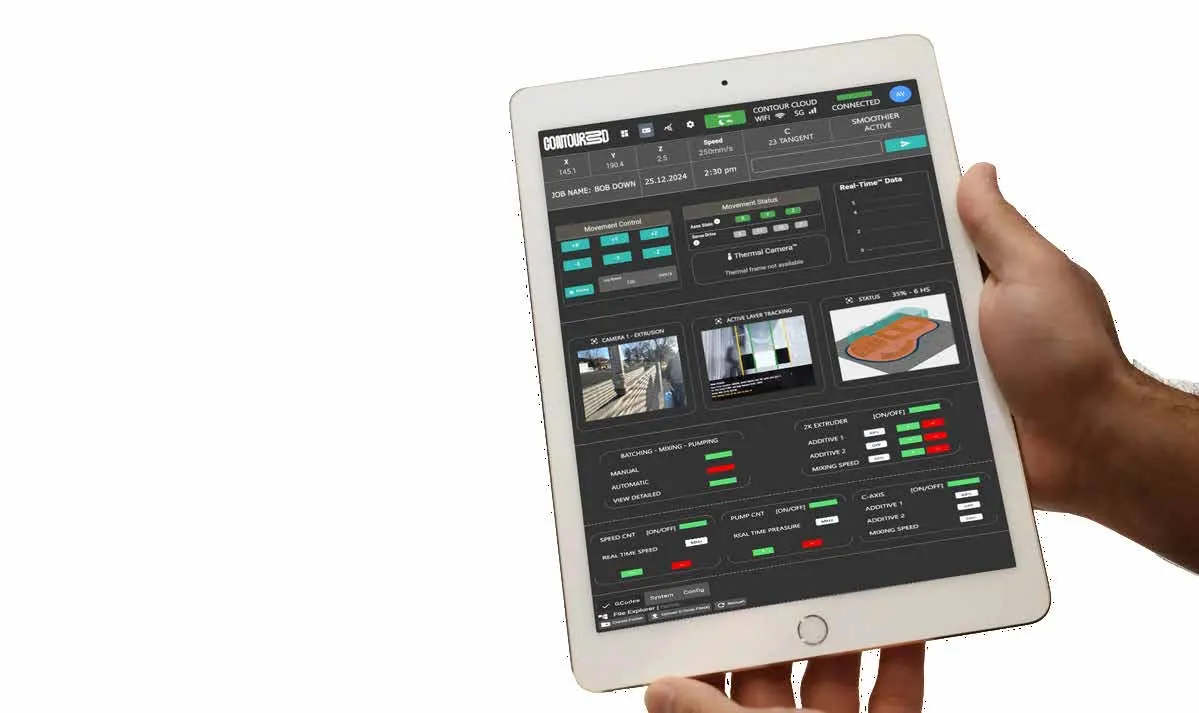
Watch it, and control it, from anywhere.
Follow the print live from your phone or tablet: camera feeds and a real-time digital twin, wherever you are. Over Starlink or 5G our team can take control of the printer and support it remotely, whether the job is on site or in the factory.
Remote support from our team
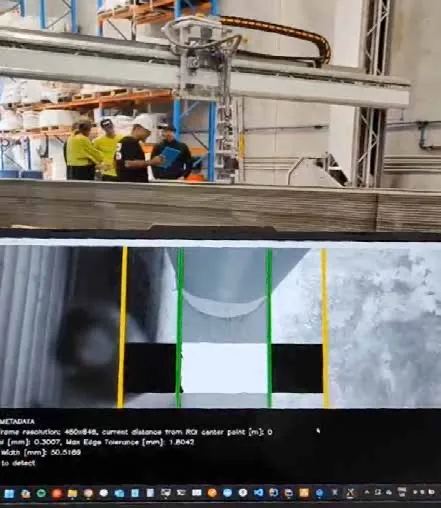
Each print helps improve the next.
Each printer streams its own data back. Machine vision watches the print for faults while the system tracks weather, site conditions and print speeds as the job runs. That data is used to refine the recommended settings for the next one.
Everything in one place.
One login carries the whole job, from the first quote to the as-built record.
Secure client login
A private, encrypted account for every client and project.
Real-time digital twin
A live twin of the build, kept as the as-built record.
Site photos, auto-filed
Snap photos on site and they upload straight to the job or quote.
Resource library
Documentation and how-to instructional videos in one place.
Instant reports
Recent, active or historic prints at the press of a button.
Materials & spares
Order ContourCrete and spare parts directly from the cloud.
The material
Engineered in Australia.
ContourCrete is our own eco-friendly, 3D printable building material,
designed and made in Australia.
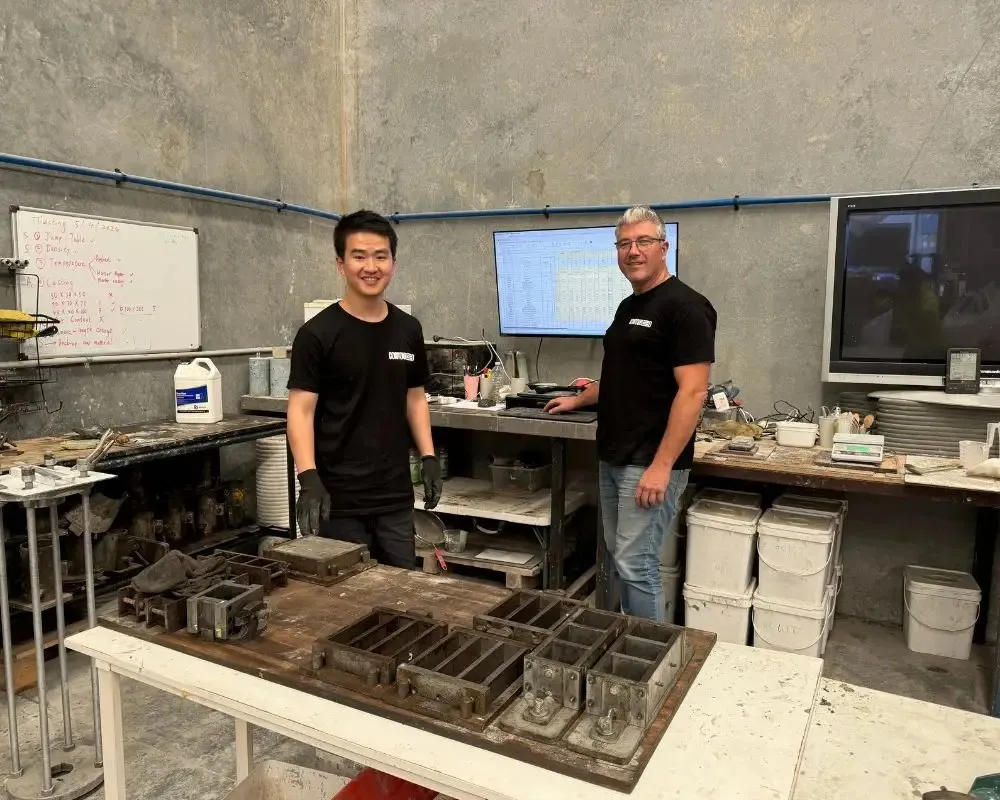
Our material scientists develop and test custom blends for each project
and location, in-house and alongside the University of New South Wales.
It reaches a high 56 MPa compressive strength with a 50+ year design
life, yet prints with the aesthetic quality to form curves and
intricate detail.
Because every aggregate is 5 mm or smaller, ContourCrete is technically
a mortar rather than a concrete.
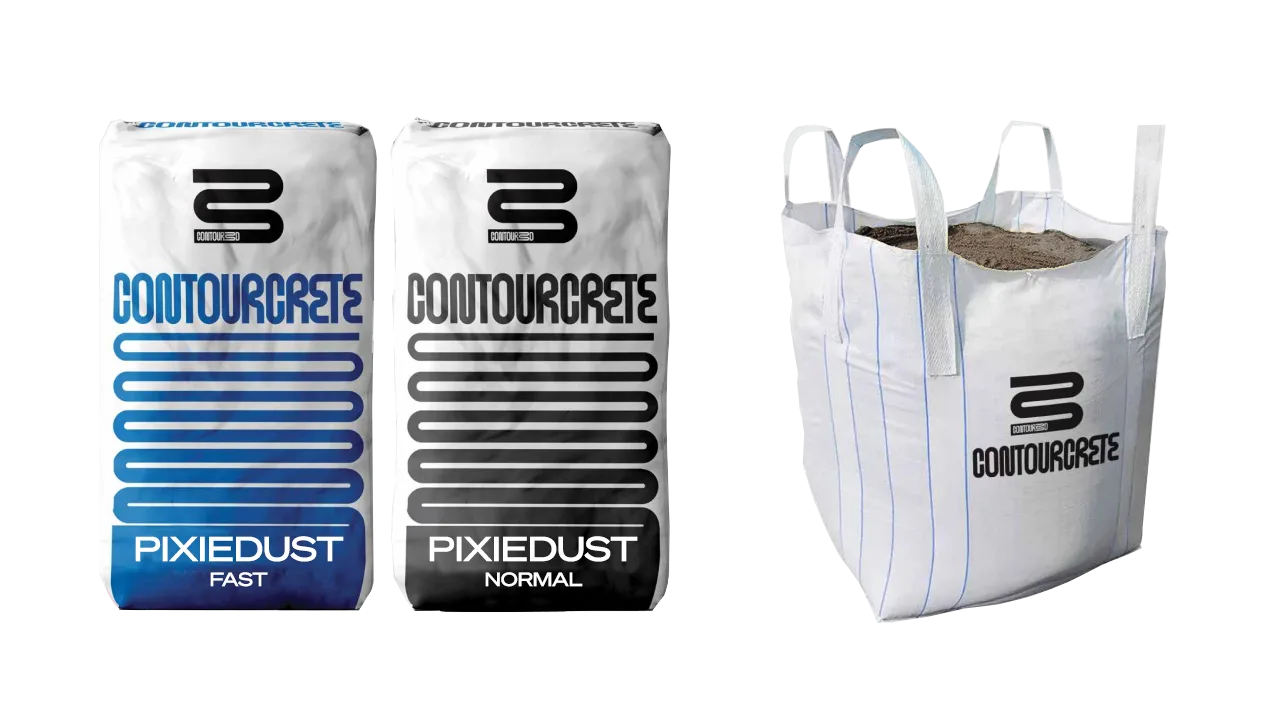
56 MPa
28-day compressive strength
~40%
recycled content, by volume
50+ yrs
design life
5 mm
maximum aggregate size
A greener mix.
Around 40% of the ContourCrete mix, by volume, is recycled content.
We turn waste streams that would otherwise head to landfill into
durable, structural walls.
The blend is tuned to each project, so typical recycled-content inputs
include:
Crushed construction waste
Crusher dust from recycled building materials
Fly ash
A by-product of power generation
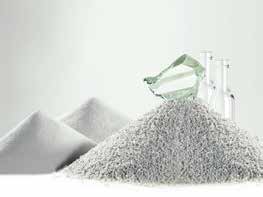
Expanded waste glass
Glass otherwise destined for landfill
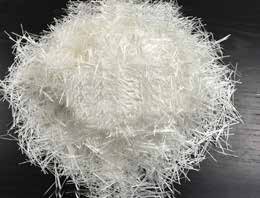
Recycled plastic fibres
Reinforcing fibres from recycled plastic
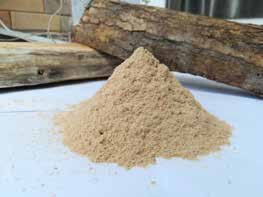
Wood flour
Waste from timber mills
Not your usual concrete.
Ordinary concrete has the wrong rheology for printing.
Wet, it simply slumps.
ContourCrete is engineered to hold its own shape.
-
Extrudes like toothpaste, holds its shape
Soft and wet as it leaves the nozzle, it carries layer after layer on top without deforming.
-
A mortar, not a concrete
Aggregates of 5 mm or less give the fine finish and printability. By definition, that makes it a mortar.
-
Set time, tuned on site
How fast the mix sets is controlled for the weather and the printing pace by our on-site systems. More on those next.
On-site systems
From mix to printed wall.
Material reaches the nozzle one of two ways.
On site we can batch a fresh mix in the TITAN mobile batching plant, or
store pre-blended dry ContourCrete in a bulk silo and mix it on demand
with the MAI Multimix 3D.
TITAN is our own machine.
The MAI Multimix 3D is made by MAI, and we are its Australian
distributor.
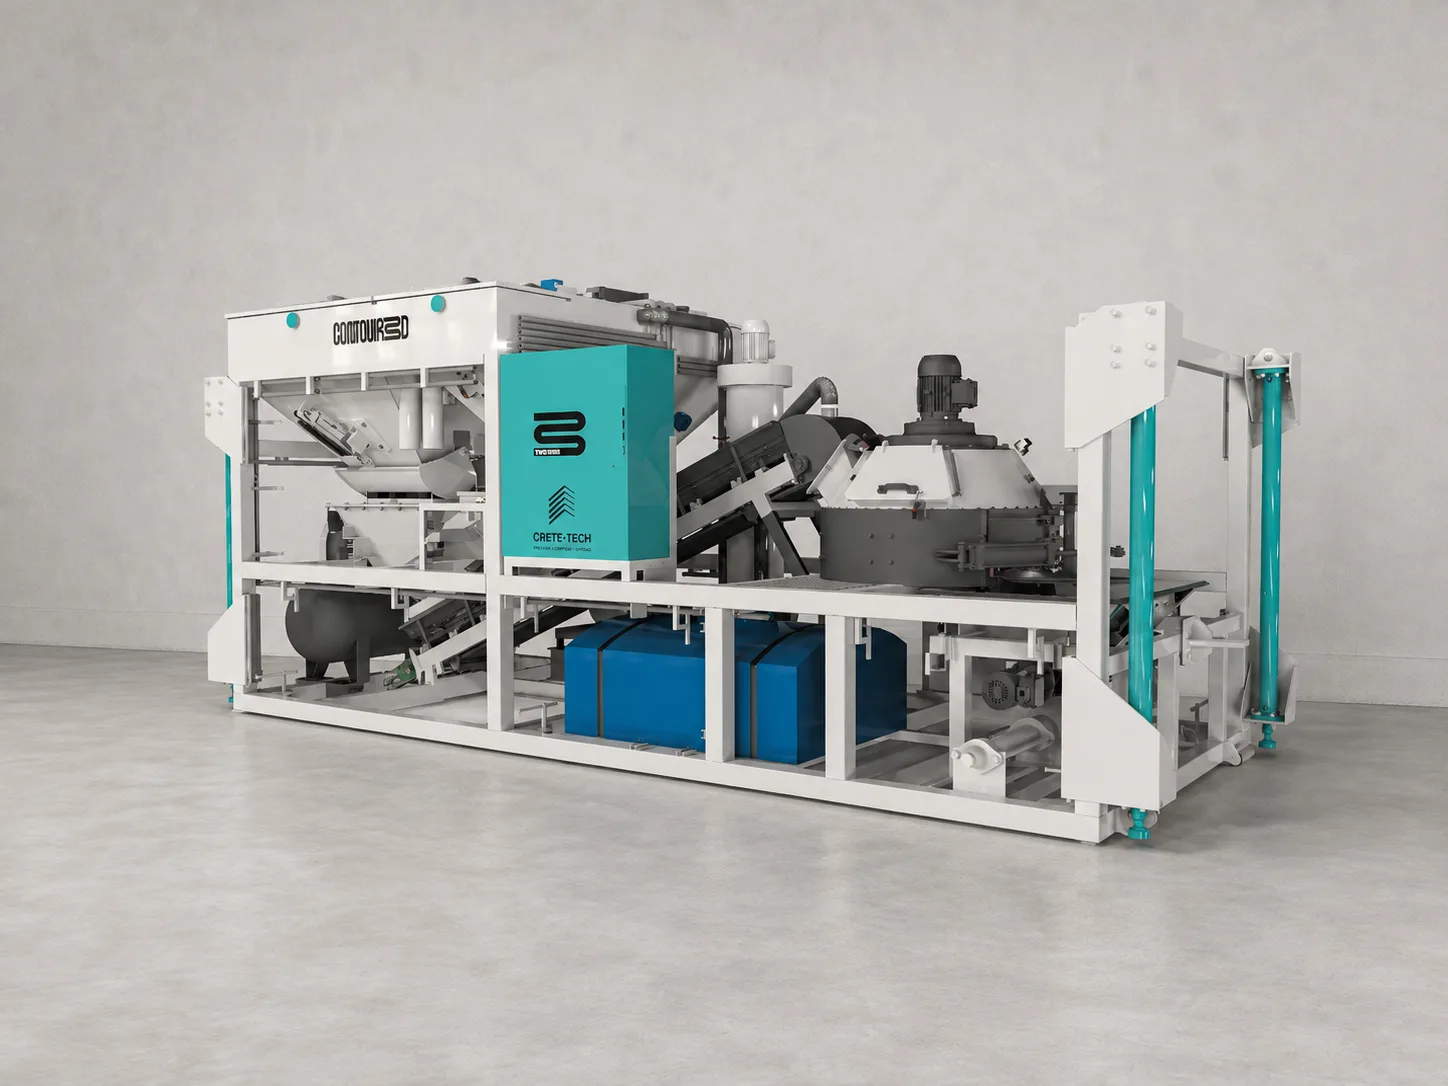
The TITAN mobile batching plant.
Our own mobile batching plant, designed and built in-house.
It batches a consistent ContourCrete mix on site and adjusts how fast
that mix sets for the weather and the printing pace, with the operator
able to override it at any point.
-
Our own machine. Designed, built and branded by Contour3D for printing.
-
Tunes the set to conditions. Helps hold quality across changing weather and print speeds.
-
Built to move. Transports on a truck and sets up fast for on-site printing.
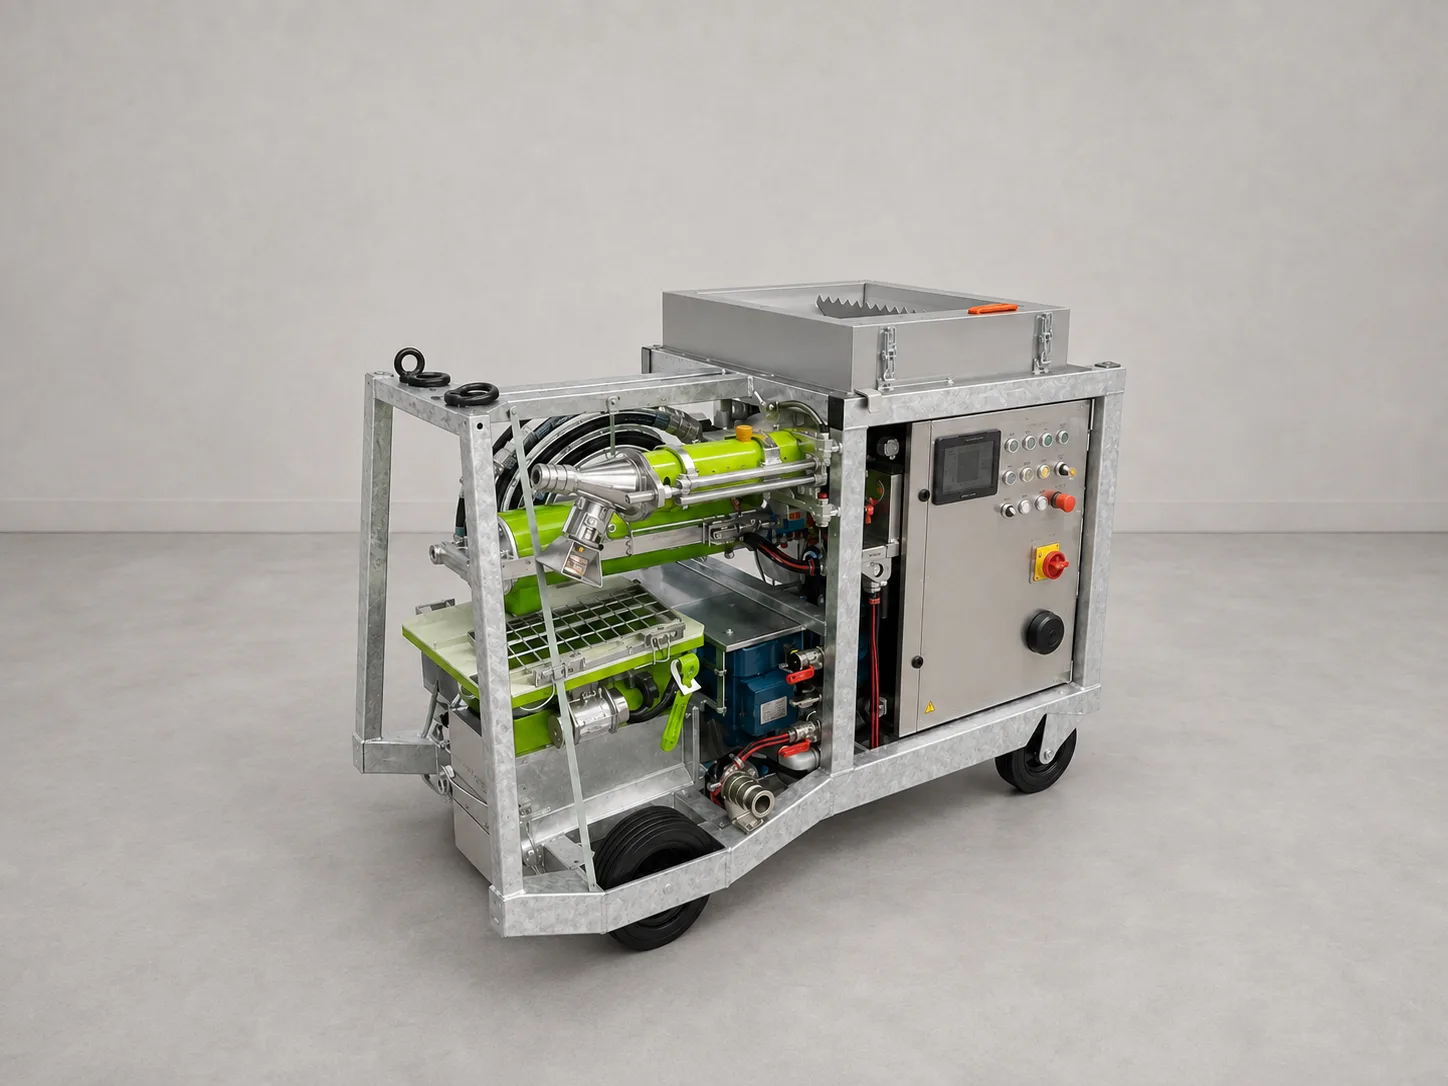
MAI Multimix 3D.
We are the Australian distributor for MAI's 3D printing range. The MAI Multimix 3D mixes dry ContourCrete with water as it runs and pumps a steady, consistent stream to the nozzle, for jobs where the TITAN plant is not the right fit.
- Mixes and pumps continuously rather than in batches.
- Digital water control for a consistent mix.
- Finely adjustable delivery rate to match print speed.
- Easy to clean and maintain.
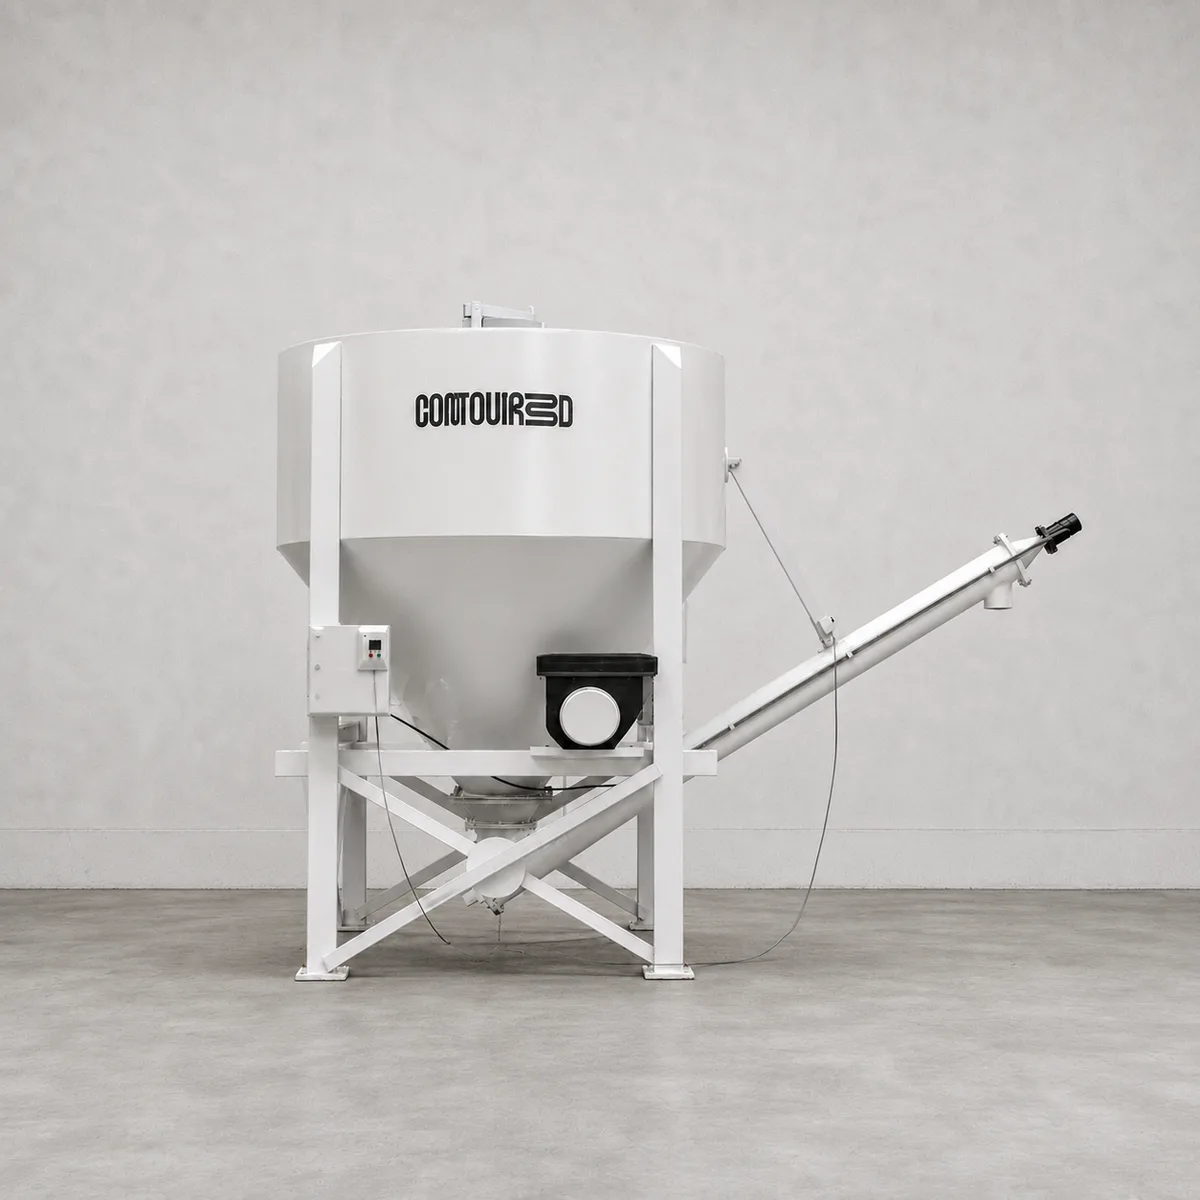
Bulk silo.
A bulk silo holds pre-blended dry ContourCrete on site, keeps it dry and free flowing, and feeds the MAI Multimix 3D continuously, so crews can print at volume without stopping to load bags.
- Stores dry batched ContourCrete in bulk.
- Feeds the mixer continuously between refills.
- Longer, more continuous prints.
- Less manual bag handling on site.
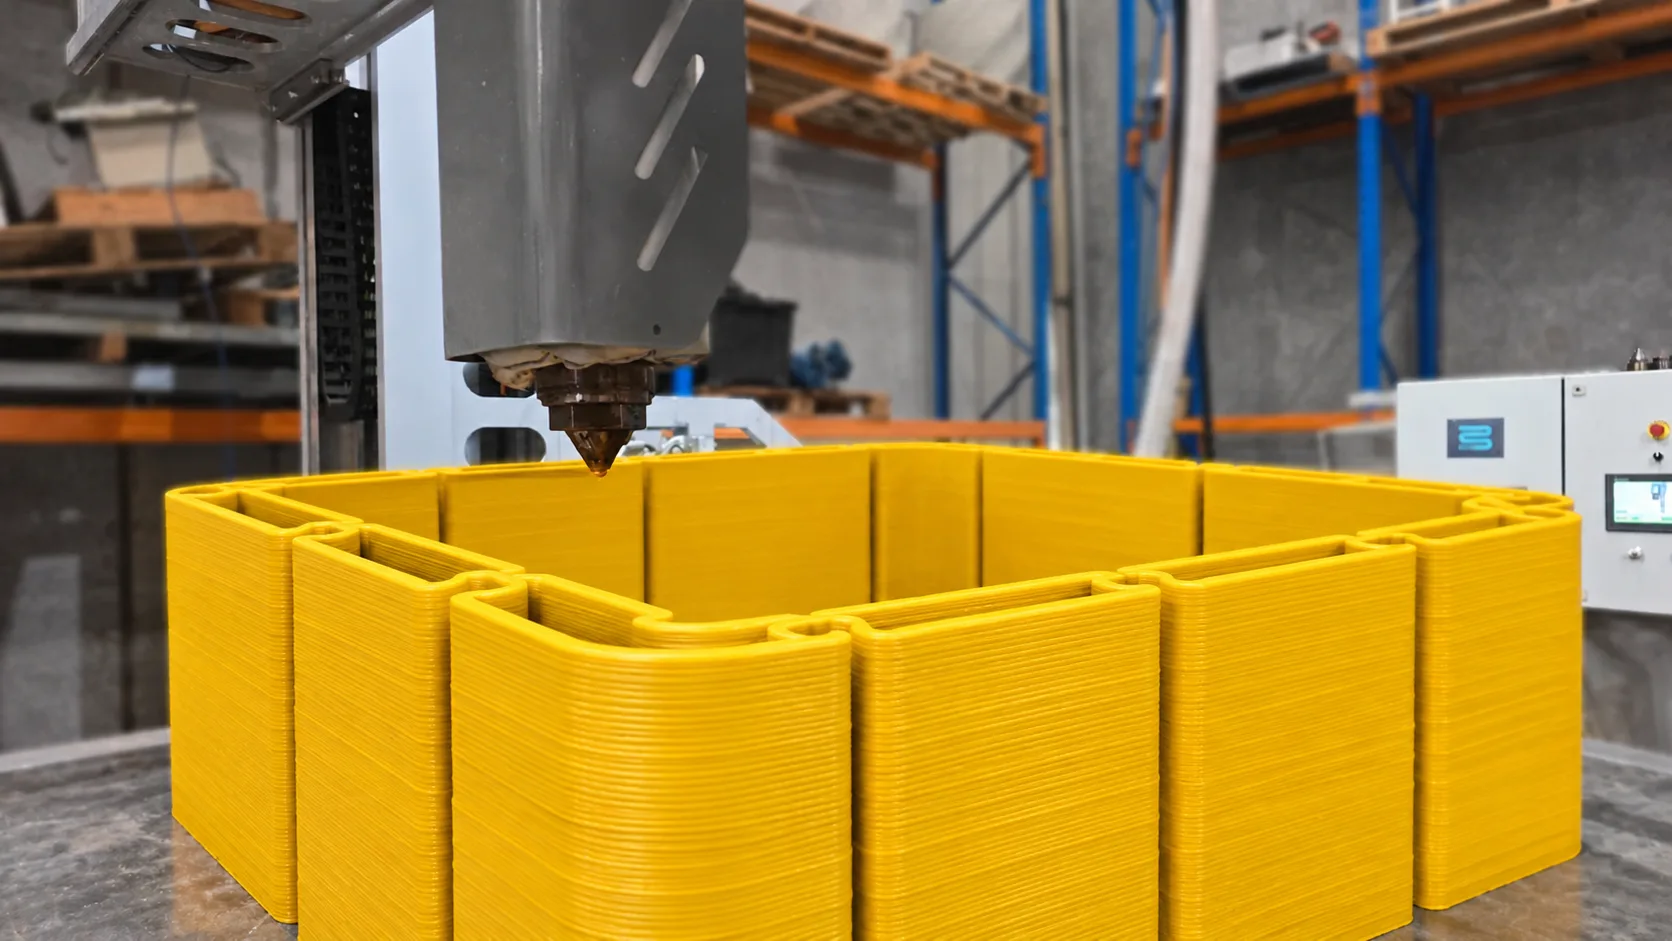
Thermoplastic printing
FeatherCrete.
We print beyond concrete.
FeatherCrete is our thermoplastic material, for lightweight
components, products and large-scale forms.
- Material
- FeatherCrete, run from virgin or recycled pellets.
- Process
- Large-format pellet extrusion, in our Sydney factory.
- Outcome
- Moulds, formwork, furniture and architectural components.
Printed in FeatherCrete
What it makes.
The pellet printer running in the factory.
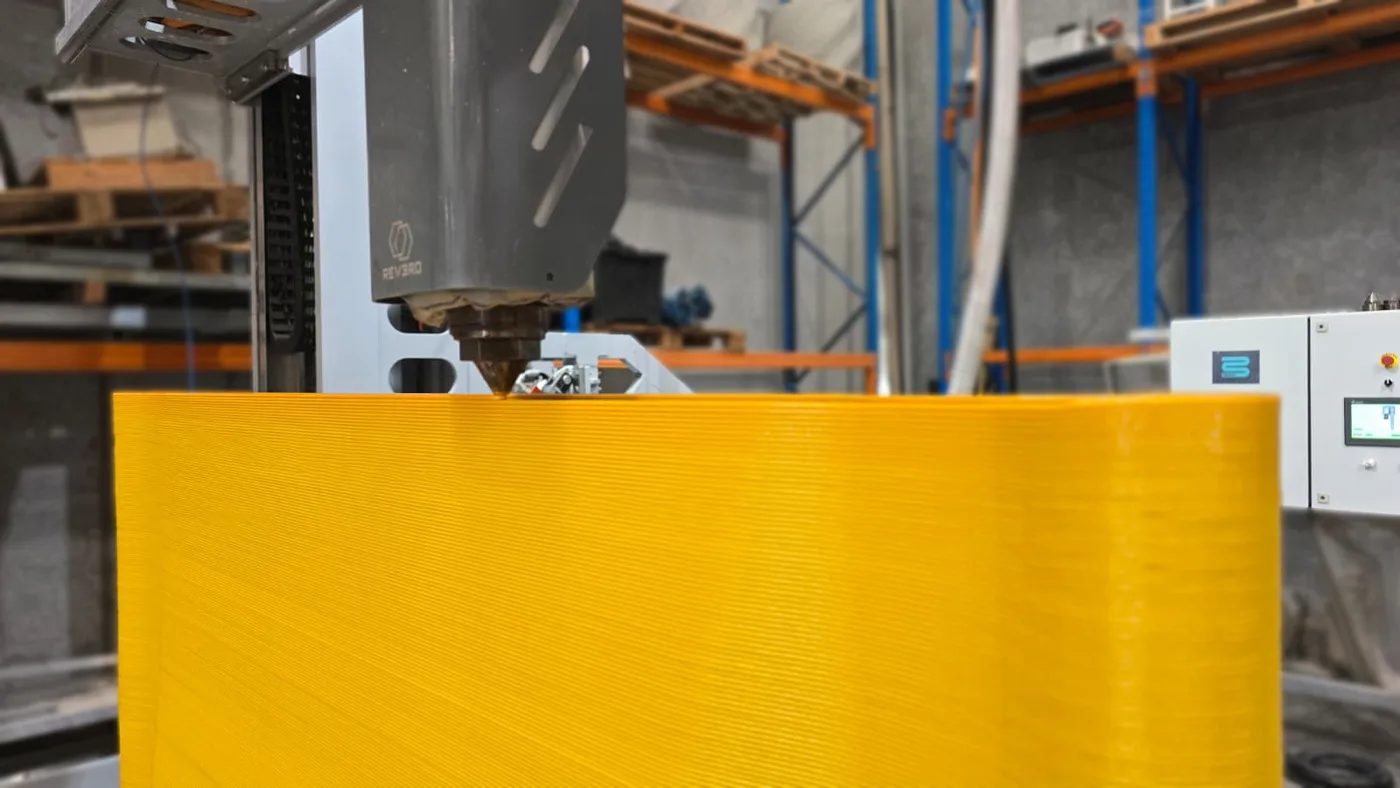
The extruder laying a panel.
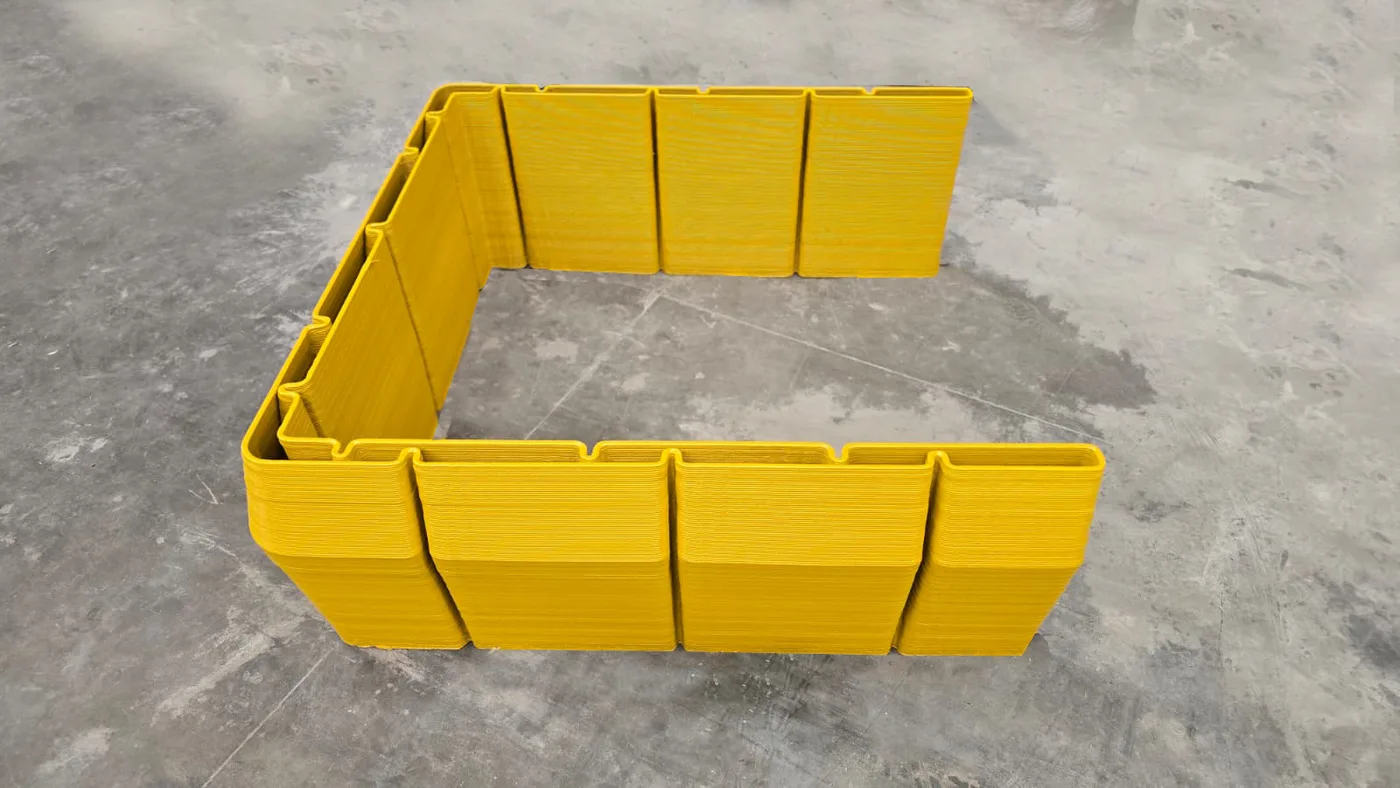
Interlocking panels, printed and assembled.